RFID Tracking in Electronics Manufacturing: WIP, Traceability and Process Control
- In electronics manufacturing, the best RFID target is often a reel container, kit, traveler, WIP carrier, serialized assembly, fixture or tool rather than every individual component.
- RFID contributes physical identity and movement events to a broader traceability record. MES, ERP, quality, test and machine systems still own process results, genealogy and authoritative production state.
- The strongest pilots focus on repeatable handoffs where search, stale WIP data or manual transactions already create measurable production friction.
Electronics manufacturing has a traceability problem that is easy to describe badly. A printed circuit board may contain hundreds or thousands of components, yet the useful RFID target is rarely every resistor, capacitor or integrated circuit on that board. The more practical question is where identity becomes difficult to maintain as material, work-in-process, tools and assemblies move between stores, kitting, production, test, inspection, rework and shipping. RFID is valuable when it removes uncertainty at those handoffs without adding another manual transaction.
Those handoffs are hard to manage in electronics because the physical product changes quickly while the information around it has to remain coherent. A reel becomes part of a kit, the kit feeds an assembly process, the assembly moves through test and inspection, and a failed unit may loop back through rework before it can continue. Production systems may know the planned route, but they still depend on people, scanners and machines to report what physically happened. RFID can automate selected observations in that chain, but it does not replace the bill of materials, machine process data, quality records or component pedigree that already belong in the MES, ERP, QMS or traceability system.
Electronics traceability is broader than component tracking
The electronics industry already treats traceability as a structured manufacturing discipline. IPC's Factory of the Future program identifies IPC-1782 as the standard for manufacturing and supply chain traceability of electronic products, covering products, processes, assemblies, parts, components and equipment used in printed board and mechanical assembly. The standard also distinguishes different levels of traceability based on risk, which is a useful reminder that not every item deserves the same identification strategy.
RFID fits inside that broader traceability model as an automated data-capture method. It can identify a reel, tote, kit, traveler, carrier, board assembly, test fixture or tool as it enters or leaves a controlled area. The event can then be reconciled with the work order, routing, lot, serial number or quality state already maintained elsewhere. A successful system therefore starts with the manufacturing record that needs to be trusted and works back from there to the items worth tagging.
This is also where electronics manufacturing differs from many warehouse applications. In a warehouse, the item being identified may remain essentially unchanged between receiving and shipping. On an electronics line, identity is transformed by consumption, assembly, test and rework. The RFID design has to follow those state changes deliberately or it will create a very detailed history of movements that still does not answer the production question.
Start with the object that survives the process step
One of the most common design mistakes in electronics is choosing a tag target that is too granular for the actual problem. If the goal is to know whether a work order reached test, the useful tag may be on the serialized assembly, a dedicated carrier or a traveler that remains with the unit. If the goal is to know whether material was delivered to a line, the tag may belong on the reel container, tote or kit rather than on each component consumed by the placement machine. The physical identity should survive long enough to support the event the business needs.
This is especially important around small parts and metal-dense electronics. Passive UHF RFID performance depends on antenna geometry, nearby conductive material, tag orientation and the surrounding read environment. A tiny tag attached directly to a board or component may have less useful read range and a more difficult radiation pattern than the same tag architecture on a carrier designed for RF performance. In many plants, the technically cleaner design is to track the container, traveler or assembly through the manufacturing flow and let the MES maintain the detailed component genealogy.
This approach is also clearer about the layer at which RFID contributes data. The reader observes a physical identity and movement event, while other manufacturing systems continue to own placement records, test results, process parameters and component-level traceability.
WIP is often the highest-value electronics use case
High-mix electronics production creates many opportunities for WIP to become difficult to see. Assemblies can wait for functional test, move to inspection, leave the normal route for troubleshooting, return to rework, or sit in a staging area while another constraint is resolved. A production planner may have a transaction showing where the unit was supposed to be while the physical assembly has already moved somewhere else. People then walk the floor, call another department, search racks or open multiple systems to reconstruct the state of one job.
RFID can reduce that gap when fixed read points are placed at transitions that already matter operationally. A read at the entrance to a test area can establish that an identified assembly arrived there. A later observation at a rework cell can show that it moved backward in the route. The software can calculate dwell time and flag an exception, but it should not infer pass or fail from location alone.
Our work-in-process tracking guide discusses the broader manufacturing architecture. In electronics, the additional design challenge is preserving the relationship between the physical assembly, its serial or work-order identity and the process records produced by automated equipment.
Honeywell shows why trustworthy WIP data matters more than the tag type
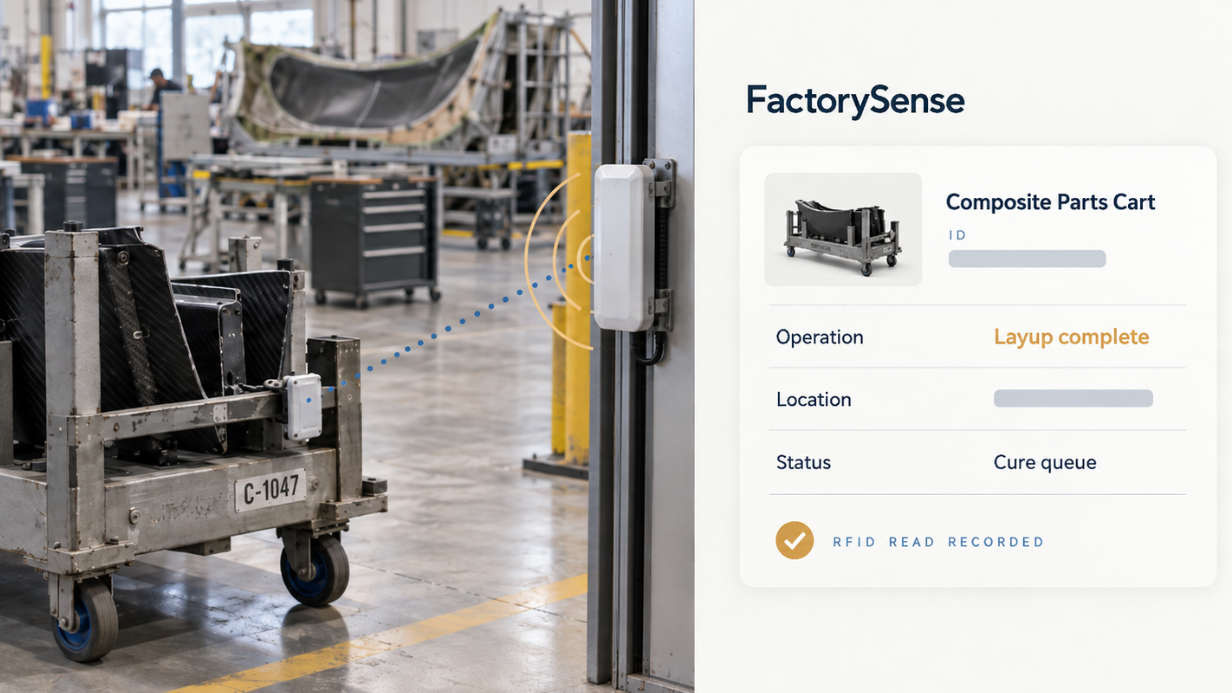
The FactorySense deployment at Honeywell Aerospace is a useful example because it began with an RFID system that was already in place but was not delivering useful production visibility. The legacy deployment used active RFID tags for WIP, yet battery maintenance, inconsistent data and coverage problems made the system difficult to trust.
FactorySense reassessed the tag performance, reader coverage, data architecture and integration model, then moved the application to passive RFID. Hardened tags and revised reader placement were paired with software that could turn reads into usable WIP and asset information. Once the system became reliable, the same infrastructure expanded beyond assemblies to mobile assets such as carts and tooling.
Passive RFID will not be the right answer everywhere. The tracking architecture has to match the object, the read environment and the manufacturing question. A lower-maintenance passive design worked well for this application because the process could be instrumented around controlled read points and the software could provide the context needed to make those observations useful.
Traceability needs a data model
A fixed reader can see the same tag many times in a few seconds. Those observations are useful to the edge software, but sending every raw read directly to an ERP or MES would bury the business system in noise. The system needs to decide whether the observations represent arrival, departure, continued presence, a likely transition, or nothing new at all.
The same issue appears in the broader digital-thread work of the National Institute of Standards and Technology. NIST's manufacturing work focuses on connecting product definitions, manufacturing activity and quality information so data can be reused and traced across the lifecycle. RFID can contribute physical events to that thread, but it is only one source among machine data, inspection results, product definitions, work instructions and enterprise transactions.
This is why integration should be designed before a plant adds dozens of read points. The team should know which system owns the object identity, which events are authoritative, what happens when an expected read is missing, and how duplicate or contradictory observations are reconciled. Those design decisions are central to connecting factory events to ERP, MES and quality systems, and our guide to connecting factory data to business systems covers that event-processing layer in more depth.
Material visibility and component genealogy are different records
Electronics manufacturers often want better visibility into reels, trays, moisture-sensitive material, high-value components and line-side kits. RFID can help locate or confirm the movement of those material containers, particularly when the current process depends on manual scans or paper moves. It can also reduce search and reconciliation effort when material is staged in multiple areas or moves between stockrooms and production.
RFID does not, by itself, prove that every component on a reel was placed on a particular board. That genealogy usually comes from placement equipment, feeder setup, barcode or machine-level identification, MES records and other process data. An RFID event can strengthen the chain by showing that a reel or kit reached the expected area, but the manufacturing system still needs the evidence that consumption actually occurred.
That boundary is important for quality investigations. If a suspect lot has to be traced, the plant needs a record that can connect the affected material to the assemblies that actually consumed it. RFID may make one or more physical handoffs easier to capture, while the detailed build record remains a composite of data from multiple systems.
Tools, fixtures and test equipment are a different tracking problem
Test fixtures, programming equipment, calibration standards, carts and specialized tools can be better RFID targets than small electronic components. These assets are reusable, physically mobile and often valuable enough that search time or uncertainty about availability affects production. They also tend to offer more freedom for tag placement and antenna design than a populated circuit board.
The operational questions are straightforward: where was the fixture last seen, which area currently has it, was a calibrated instrument issued to the correct work cell, and did a shared cart return from another line? Fixed readers can capture repeatable transitions, while handheld RFID can support a search when continuous fixed coverage is unnecessary. The technology choice should follow the question instead of forcing every asset into the same tracking mode.
Calibration status itself should continue to come from the calibration or quality system. RFID can identify the instrument and automate custody or location events, but a radio read is not evidence that calibration was performed. Good implementations keep those responsibilities separate while presenting the operator with one coherent answer.
Test, inspection and rework require careful event semantics
Electronics manufacturing includes process states that are easy for a location system to misinterpret. A board sitting inside the test area may be waiting, actively being tested, held for engineering review, or already failed and awaiting rework. Physical location is useful context, but it is not the quality disposition. Treating the two as interchangeable creates confident-looking data that is wrong in exactly the situations where traceability matters most.
A stronger design uses RFID to establish the physical handoff and another system event to establish the process result. For example, RFID may record that serial 123 entered functional test at 10:14, while the test system records the actual result at 10:23. If the assembly then appears at rework, the tracking history adds physical continuity without inventing a quality decision.
This also makes exception handling much clearer. If the MES says the job passed test but the tagged assembly never appears at the next controlled point, that discrepancy is worth investigating. If the RFID system sees an assembly near a test antenna but the test system has no record, the system should not create a pass event from proximity alone.
RF environments around electronics need to be engineered
Electronics facilities are not automatically easy RFID environments simply because the product is small. Metal benches, racks, populated boards, shielding, machinery and densely packed material can alter tag behavior and create unintended reads. Antennas that cover too much area can be as problematic as antennas that miss tags, because a production event is only useful when the system can tell which process area actually observed the item.
Tag selection therefore has to be tested on the real object, in the real orientation and at the intended process point. Reader power, antenna placement and event timing should be tuned around the physical workflow rather than around the maximum possible read distance. A successful pilot proves that tags can be read and that the system does not routinely capture neighboring work and assign it to the wrong state.
The same principle applies to heat and process exposure. A tag on a carrier that never enters a reflow oven has a different design requirement from a tag intended to remain on an assembly through thermal processes. The RFID architecture should avoid demanding extreme tag performance when the process can be instrumented more simply at the container or traveler level.
How to choose an electronics RFID pilot
A good pilot starts with a production question that is already expensive to answer manually. Examples include assemblies that routinely disappear between test and rework, kits that are difficult to reconcile at line side, shared fixtures that delay setup, or WIP transactions that lag the physical floor. The pilot should be narrow enough that the team can instrument the handoffs, measure the existing delay and compare the result after automation.
The metrics should reflect the operational problem. Useful measures include time spent searching, time between physical movement and system update, number of WIP location discrepancies, dwell time in a selected queue, fixture availability, and the percentage of expected transitions that generate a valid business event. Read rate still matters, but it is an engineering metric in service of those outcomes.
The final test is whether production trusts the answer. An RFID deployment that occasionally misses a read can often be engineered and improved. A deployment that routinely assigns the wrong process state is more damaging because users stop relying on it and return to manual verification. Our guide to why RFID systems fail explains how those RF, event-logic and integration failures should be diagnosed. The aim is a smaller number of manufacturing events, each accurate enough to remove work from the process.
Where RFID fits in an electronics factory
RFID is strongest in electronics manufacturing when it connects a durable physical identity to a process transition that the business already cares about. That may mean tracking a reel container into kitting, a serialized assembly into test, a WIP carrier into rework, or a fixture between work cells. The detailed product history still comes from the combination of material, machine, quality and enterprise records.
That is a narrower role than the old smart-factory pitch promised. RFID does not need to predict every problem or create a digital twin by itself; it needs to make selected physical events observable with less labor and less ambiguity, then deliver those events to the system where someone can act on them.
For electronics manufacturers evaluating RFID, a useful starting question is where the digital production record most often falls behind physical reality. If the answer is a repeatable handoff involving WIP, material containers, tools or test assets, RFID may be a strong fit. If the problem is component genealogy inside an automated assembly machine, process capability, or test quality, another data source probably owns that answer.
Sources and further reading
Can RFID track individual electronic components?
Sometimes, but individual component tagging is often unnecessary or impractical. Small size, metal content, dense packaging and the need for detailed consumption genealogy may make a reel, tray, kit, carrier or assembly a better RFID target. Placement equipment and MES records are usually better sources for proving exactly which components were installed on a board.
Can RFID be used around printed circuit boards and metal equipment?
Yes, but the RF design has to be tested on the real object and in the real production environment. Nearby metal, populated boards, racks and machinery can change tag performance, so tag selection, placement, antenna geometry and reader power should be validated at the intended process point.
Does an RFID read prove that a board passed inspection or test?
No. An RFID read can show that an identified item was observed at a controlled location or transition. Test results, inspection disposition and process completion should come from the system or equipment that actually performed and recorded that activity.
What is a good first RFID use case in electronics manufacturing?
Start with a repeatable problem where the physical state is hard to determine and the uncertainty already costs time. Common candidates include WIP between test and rework, line-side kits, shared fixtures, mobile carts, calibrated tools and high-value assemblies moving between major process areas.
Schedule a complementary working session with an RFID professional to discuss your floor or yard, your systems of record, and where the visibility gap between them is costing you.
Book a session