The Benefits of Using RFID Technology in the Manufacturing Industry: A Data-Driven Perspective
- RFID creates value by reducing the gap between physical reality and the system record, not simply by replacing barcode scans.
- The research suggests that item-level information becomes more valuable as process variability, complexity and the cost of mistakes increase.
- The strongest business cases start with an operational uncertainty the company is already paying to manage through search, counting, reconciliation, buffers or manual transactions.
RFID is often presented to manufacturers through a familiar list of benefits: better inventory accuracy, lower labor costs, improved traceability, fewer errors and greater efficiency. Those outcomes are all possible, but the list does not explain much. It tells you what might get better without explaining why identifying a physical object by radio should change the economics of a factory in the first place.
The research points to a more useful way to think about it. RFID creates value when it reduces the gap between what is physically happening in an operation and what the systems used to run that operation believe is happening.
That gap is everywhere. A work order moves to the next operation, but the transaction does not get entered until later. A fixture is returned to a different location. Material reaches a workstation while the ERP still shows it upstream. A calibrated tool is somewhere in the building, but nobody knows where. Inventory exists physically, just not where the system expects it to be.
These are different operational problems, but they have the same underlying characteristic: physical reality has moved ahead of the digital record. RFID is useful because, in the right process, it can close that gap without asking somebody to stop what they are doing and create the record manually.
A more current operating record
Manufacturing systems are generally good at recording transactions. They are not necessarily good at observing physical reality.
An ERP may know that material was issued to a work order. An MES may know that an operation is scheduled. A warehouse system may know the bin where a part was last assigned. None of those records proves where the physical item is now, and the distinction becomes important as soon as the item begins moving faster than people update the system.
Researchers Hongyan Dai and Mitchell Tseng described inventory inaccuracy as the mismatch between physical inventory and the record maintained by the information system. Their analysis matters because the cost is not confined to the missing or misplaced item. Once the record is wrong, that error can influence replenishment, shortages, inventory holding and other decisions downstream.1
That is the first thing I would look for when evaluating an RFID project. Not “Can we collect more data?” but “How long are we currently making decisions from a version of reality that is already stale?”
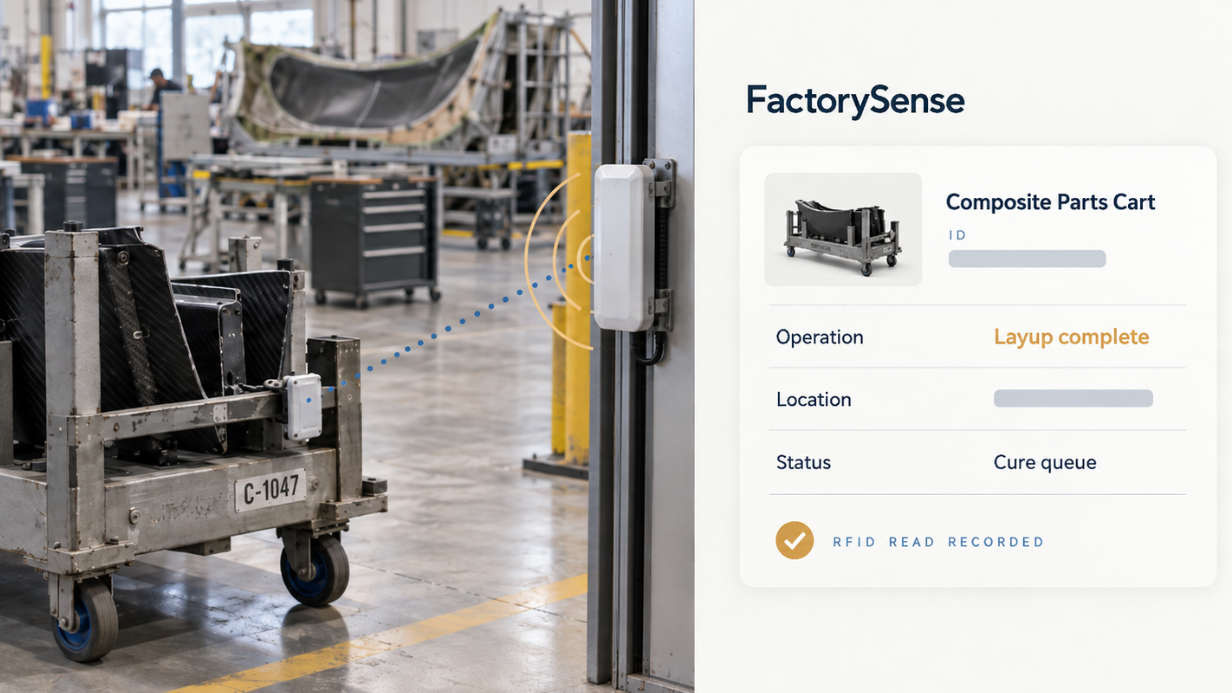
NIST addresses a related issue in its work on the manufacturing digital thread. Modern manufacturing increasingly depends on information moving among engineering, production, quality and support functions, but the information often remains fragmented across systems. The objective of the digital thread is to make those records usable as part of a connected product and process history.2 RFID can give the physical object a reliable place in that history. A tagged item crossing a read point becomes a timestamped event. Depending on the process, that event might update inventory, advance a work order, change location, trigger an exception or simply become another point in the item's history.
The read itself is almost never the valuable part. The value comes from what the business is able to know or do because the read occurred.
Labor that exists only to keep the system informed
This is one of the easiest places to misunderstand RFID.
RFID does not inherently make someone better at machining a part or faster at completing an inspection. What it can remove is the work surrounding those activities whose only purpose is to keep the information system current.
Take a traveler moving between operations. If an employee has to stop, find the barcode, scan it and confirm the transaction, that work does not improve the product. It exists because the system otherwise has no way of knowing that the work moved. The same is true when someone checks a tool out of a crib, records a material transfer, counts containers or walks the floor looking for something because nobody trusts the last recorded location.
Researchers at Cambridge, Adelaide and the Institute for Manufacturing examined RFID through the framework of the Toyota Production System's seven wastes. They identified automated data collection, stronger data dependencies and better production and inventory visibility as ways RFID could support leaner operations.3 That framing is much more useful than saying RFID “saves labor,” because it forces you to identify the labor you are actually trying to remove.
A practical question is simply: what are people doing today only because the software cannot observe the physical event itself?
Sometimes the answer is “not much.” If an operator already has the item in hand and a barcode scan takes almost no extra effort, the economics may be perfectly acceptable as they are. There is no reason to replace a dependable process just because RFID is available. The case gets stronger when the reporting step is itself creating friction.
Work-in-process visibility is partly a measurement problem
The obvious value of WIP tracking is that people spend less time looking for things. That is real, but it understates the opportunity. Once movement is recorded consistently, the history of that movement becomes useful in its own right.
A 2013 study of a discrete manufacturer used RFID-based real-time location data to observe products moving through a quality-control process. Researchers were able to calculate cycle time, processing time, movement speed and other shop-floor measures at a level of detail the company's previous measurement methods did not provide. The manufacturer then used that information to identify bottlenecks and evaluate a redesigned workflow.4
What I find interesting about that study is that RFID created value before it automated much of anything. It first made the existing process easier to see.
Most plants can tell you how many units were completed yesterday. Fewer can tell you, with confidence, where material spent the previous six hours, which route it actually took, where it waited, or which stage introduced the variability that eventually showed up as a late order. If the only transactions happen at the beginning and end of a process, the middle tends to become anecdotal. People know where work usually goes. They know where it is supposed to go. They may even know where it probably went. That is not the same as having a history of what actually happened.
We have seen the same basic problem in FactorySense deployments. At CAES Systems by Honeywell, the issue was not simply that work in process could be hard to locate. The larger problem was that the legacy system did not provide a sufficiently useful or trusted picture of carts, assemblies and tools moving through production. Reworking the deployment around passive RFID gave the operation a better record of what was happening on the floor without depending on employees to maintain that record manually. Read the CAES/Honeywell WIP case study.
Sometimes the real benefit is that the factory can operate differently
Some of the more interesting academic work on RFID does not ask whether it makes an existing process cheaper. It asks whether better automatic information makes a different production strategy possible.
Kurt Hozak and David Collier modeled RFID and barcode tracking in job-shop manufacturing and looked specifically at lot splitting. Their results showed that extensive lot splitting could hurt performance when the process depended on barcode tracking, while automatic RFID traceability could support operating policies that improved flow time and tardiness.5
That has a fairly important implication. Manufacturers often want smaller transfer batches, more dynamic routing, more granular WIP control and more responsive scheduling. But every increase in operational granularity creates additional information requirements. If every additional movement also requires another scan, another transaction or another handwritten update, the effort required to maintain the record can eventually become part of the constraint.
Automatic identification changes that tradeoff.
This is why I would be careful about evaluating RFID as if it were simply a replacement for a barcode scanner. In some environments that is exactly what it is, and the business case may be weak. In others, it becomes infrastructure that allows the plant to manage at a level of detail that would be impractical if every movement had to be reported manually.
Inventory accuracy matters because the rest of the business trusts the number
Inventory accuracy is often discussed as though it were a self-contained metric. It is not. Purchasing uses it. Scheduling uses it. Replenishment logic uses it. Customer commitments may ultimately depend on it.
When the physical quantity and the system quantity diverge, the consequences travel.
Some of the strongest field research on RFID and inventory accuracy comes from retail, not manufacturing, which means the percentages should not be copied into a factory ROI model. Still, the pattern in the results is extremely instructive.
In experiments published in Production and Operations Management, Hardgrave, Aloysius and Goyal found an approximately 26% reduction in inventory-record inaccuracy in one field experiment. In a larger experiment across five product categories, however, the outcomes varied dramatically. Some categories showed no statistically significant improvement, while another improved by as much as 81%.6
That range tells us more than the average does. The value of RFID depends heavily on what is wrong before it arrives. If the existing process already keeps highly accurate records, there may be little for the technology to correct. If the operation is full of missed transactions, informal movement, misplaced items and distrust of the system quantity, the opportunity is much larger.
An industrial study involving more than 10 million parts and roughly 10,000 part types found something similar from a different angle. Researchers testing fixed UHF RFID in receiving and shipping reported read rates above 99% in the processes they studied, and found that combining RFID with lean process changes reduced operating time further than lean changes alone.7
The more useful conclusion is that baseline condition matters enormously. If you do not understand what is inaccurate, delayed or expensive before the project begins, there is no meaningful way to predict what RFID will improve.
Complexity increases the value of knowing exactly what happened
One of the more useful findings in the literature concerns process variability.
Wei Zhou and Selwyn Piramuthu examined item-level information in manufacturing quality control and found that its value increased as variance in the manufacturing process increased, although that benefit was ultimately bounded.8 Gaukler and Hausman's work on mixed-model automotive assembly points in the same direction. Their research found greater potential RFID value in fast-moving, complex assembly environments where idle time is limited and mistakes or rework are expensive.9
There is a practical lesson buried in those papers: the best RFID candidate is not necessarily the thing that is easiest to tag. I would look first at the places where uncertainty is expensive.
A highly stable process with predictable routing, reliable barcode transactions and little variation may not have much to gain. The information is already good enough to operate the process. A facility with many work orders moving simultaneously, variable routing, expensive components, frequent exceptions and costly rework is different. There, the identity and state of an individual item matter more because more consequential decisions are being made from that information.
Volume matters, but complexity may matter more.
Quality and traceability are really about preserving identity
RFID does not inspect a weld, measure a dimension or determine whether a component meets specification. Its role in quality is more basic: it helps preserve the identity of the physical item as that item moves through the operations that generate the quality record.
That identity becomes the thread connecting material certifications, inspection results, operator actions, process parameters and dispositions. If the association between the physical item and those records breaks somewhere along the way, the quality data may still exist, but its usefulness declines quickly. Every manual handoff is an opportunity for that association to become weaker.
NIST's work on the digital thread is relevant here because the larger objective is to connect design, manufacturing and quality information across the product lifecycle.2 RFID can provide a persistent physical identity around which those records are organized. This becomes especially important in processes where the thing being tracked changes form as it moves through production. A raw material lot becomes a cut kit, then a subassembly, then part of a finished product. The physical object has changed, but the business still needs to reconstruct what went into it, what happened to it and what evidence supports its acceptance.
In a FactorySense deployment for a medical-device manufacturer, fixed RFID reads were used to capture WIP movement while the tracking data was integrated with existing enterprise systems. The useful result was not simply a dot on a map. It was a stronger record of how the item had moved through production. See the medical-device manufacturing case study.
The same principle applies in composite manufacturing, where lot history, expiration, processing and finished-part genealogy all have to remain connected as materials move through multiple stages. See the composite-material traceability case study.
Asset tracking follows a different economic logic
Asset tracking has a different cost structure from inventory tracking because the thing being tracked is usually not consumed, sold or written off on a predictable cycle. A tool, fixture, gauge or piece of mobile equipment may remain in the business for years, move among departments without a formal transaction, require periodic calibration, and become operationally unavailable long before anyone considers it truly lost.
That makes the economic impact harder to see in a general ledger. The cost often appears indirectly: technicians spend time searching, production waits for a missing fixture, another tool is purchased because the first one cannot be located, or a calibrated asset reaches its due date while sitting somewhere outside the normal control process. None of those events necessarily looks like an “asset tracking” expense, but together they can create a meaningful amount of avoidable cost and disruption.
The scale of the physical environment matters as well. At Northrop Grumman's Space Park, FactorySense deployed RFID asset tracking across approximately 1.5 million square feet and 46 buildings. In an environment that large, an asset does not need to leave the campus to become effectively unavailable. If a team knows that a piece of equipment exists but cannot determine which building, lab or work area contains it, the operational problem is already real. Read the Northrop Grumman case study.
The same principle becomes more valuable when location is combined with other information about the asset. In another FactorySense deployment for a global industrial-equipment manufacturer, RFID location data was tied to calibration management so that the system could answer not only where a tool was, but whether it was still eligible for use. That changed the practical value of the location record. A supervisor no longer had to treat asset location and calibration status as two separate searches across different systems. Read the asset and calibration case study.
This is an important distinction when evaluating an RFID asset-tracking project. Knowing where something is can eliminate search time, but the larger value often comes from joining location to the other facts that determine whether the asset is actually usable: ownership, assignment, calibration status, maintenance condition, movement history or restrictions on where it is allowed to go.
A torque wrench sitting in Building 3 is a location record. Knowing that the same wrench is in Building 3, assigned to the correct production group and due for calibration next week is operational information.
RFID is probably better understood as uncertainty reduction
“Tracking technology” describes RFID accurately enough, but it does not really explain why companies pay for it. A better way to think about the technology is as a means of reducing uncertainty about physical operations.
The uncertainty may be about whether inventory exists, where a work order is, whether material crossed a process boundary, which component entered an assembly, where a calibrated asset moved, whether a shipment contains what the ERP says it contains, or how long work sat between two operations. When the answer is unknown, people compensate. They search, count, scan, reconcile, expedite, carry extra inventory or make assumptions.
That compensating behavior is often where the economic value is hiding.
This is also why two superficially similar RFID projects can produce very different returns. A predictable process with reliable records contains relatively little uncertainty to remove. A complicated operation with constant movement, exceptions, parallel workflows and expensive mistakes contains much more.
The tag may cost the same in both places. The information it produces is not worth the same amount.
More data will not rescue a poorly defined process
There is an important caution in the implementation research.
Ngai and colleagues studied an RFID-based manufacturing process-management implementation and identified a range of factors associated with success, including cost-benefit evaluation, management support, user involvement, staff competence, vendor selection and compatibility with the existing operation.10 That sounds less exciting than the RFID hardware, but it is closer to how projects actually succeed or fail.
A reader can generate enormous volumes of technically correct data without improving anything. The system still has to know which objects matter, which movements represent real business events, which reads should be ignored, what should change in the ERP or MES, and what somebody needs to do when the physical process does not behave as expected. If those decisions are vague, more reads simply produce more ambiguity.
This is why I would start an RFID project with an operational question rather than a hardware question: What do we need to know about the physical operation that we cannot reliably know today?
Once that question is answered, the architecture becomes much easier to reason about.
The benefits are real, but they are not universal
The research does not support a universal claim that RFID reduces labor by a certain percentage, raises inventory accuracy to a particular level or delivers a standard payback period.
What it supports is more useful. RFID can materially improve manufacturing where incomplete, delayed or unreliable information about physical objects is creating waste elsewhere in the operation. That tends to be the case when data collection is manual, physical movement happens more frequently than the system is updated, WIP routing is complex, inventory records are distrusted, search time is significant, traceability has to be reconstructed after the fact, or mistakes and rework are expensive.
Those conditions have something in common: the business is spending time or money because it does not know enough about what is happening physically. RFID can make more of that activity observable without asking people to stop the process and report it manually.
That, more than any single percentage improvement, is the manufacturing benefit worth understanding.
References
- Dai, H. & Tseng, M.M. (2012). “The impacts of RFID implementation on reducing inventory inaccuracy in a multi-stage supply chain.” International Journal of Production Economics, 139(2), 634–641. DOI: 10.1016/j.ijpe.2012.06.005.
- Hedberg, T.D., Bajaj, M. & Camelio, J.A. (2019). “Using graphs to link data across the product lifecycle for enabling smart manufacturing digital threads.” National Institute of Standards and Technology. NIST publication.
- Brintrup, A., Ranasinghe, D. & McFarlane, D. (2010). “RFID opportunity analysis for leaner manufacturing.” International Journal of Production Research, 48(9), 2745–2764. DOI: 10.1080/00207540903156517.
- Arkan, I. & Van Landeghem, H. (2013). “Evaluating the performance of a discrete manufacturing process using RFID: A case study.” Robotics and Computer-Integrated Manufacturing, 29(6), 502–512. DOI: 10.1016/j.rcim.2013.06.003.
- Hozak, K. & Collier, D.A. (2008). “RFID as an Enabler of Improved Manufacturing Performance.” Decision Sciences, 39(4), 859–881. DOI: 10.1111/j.1540-5915.2008.00214.x.
- Hardgrave, B.C., Aloysius, J.A. & Goyal, S. (2013). “RFID-Enabled Visibility and Retail Inventory Record Inaccuracy: Experiments in the Field.” Production and Operations Management, 22(4), 843–856. DOI: 10.1111/poms.12010.
- Chen, J.C., Cheng, C.H., Huang, P.B. et al. (2013). “Warehouse management with lean and RFID application: a case study.” International Journal of Advanced Manufacturing Technology, 69, 531–542. DOI: 10.1007/s00170-013-5016-8.
- Zhou, W. & Piramuthu, S. (2012). “Manufacturing with item-level RFID information: From macro to micro quality control.” International Journal of Production Economics, 135(2), 929–938. DOI: 10.1016/j.ijpe.2011.11.008.
- Gaukler, G.M. & Hausman, W.H. (2008). “RFID in mixed-model automotive assembly operations: Process and quality cost savings.” IIE Transactions, 40(11), 1083–1096. DOI: 10.1080/07408170802167654.
- Ngai, E.W.T., Chau, D.C.K., Poon, J.K.L. et al. (2012). “Implementing an RFID-based manufacturing process management system: Lessons learned and success factors.” Journal of Engineering and Technology Management, 29(1), 112–130. DOI: 10.1016/j.jengtecman.2011.09.009.
What is the main benefit of RFID in manufacturing?
The main benefit is more reliable information about physical operations. RFID can automatically capture identity, movement and location events so that ERP, MES and other systems stay closer to what is actually happening on the floor.
Does RFID always improve inventory accuracy?
No. Research shows the effect varies substantially by starting condition and product category. If records are already highly accurate, there may be little to improve; where transactions are frequently missed or items move informally, the opportunity is larger.
Where should a manufacturer start with RFID?
Start where uncertainty is expensive: WIP that is hard to locate, assets that consume search time, inventory records that are distrusted, complex traceability, or processes where manual transactions create friction.
Schedule a complementary working session with an RFID professional to discuss your floor or yard, your systems of record, and where the visibility gap between them is costing you.
Book a session