How Can RFID Help Find Lost Items in Large Manufacturing Industries?
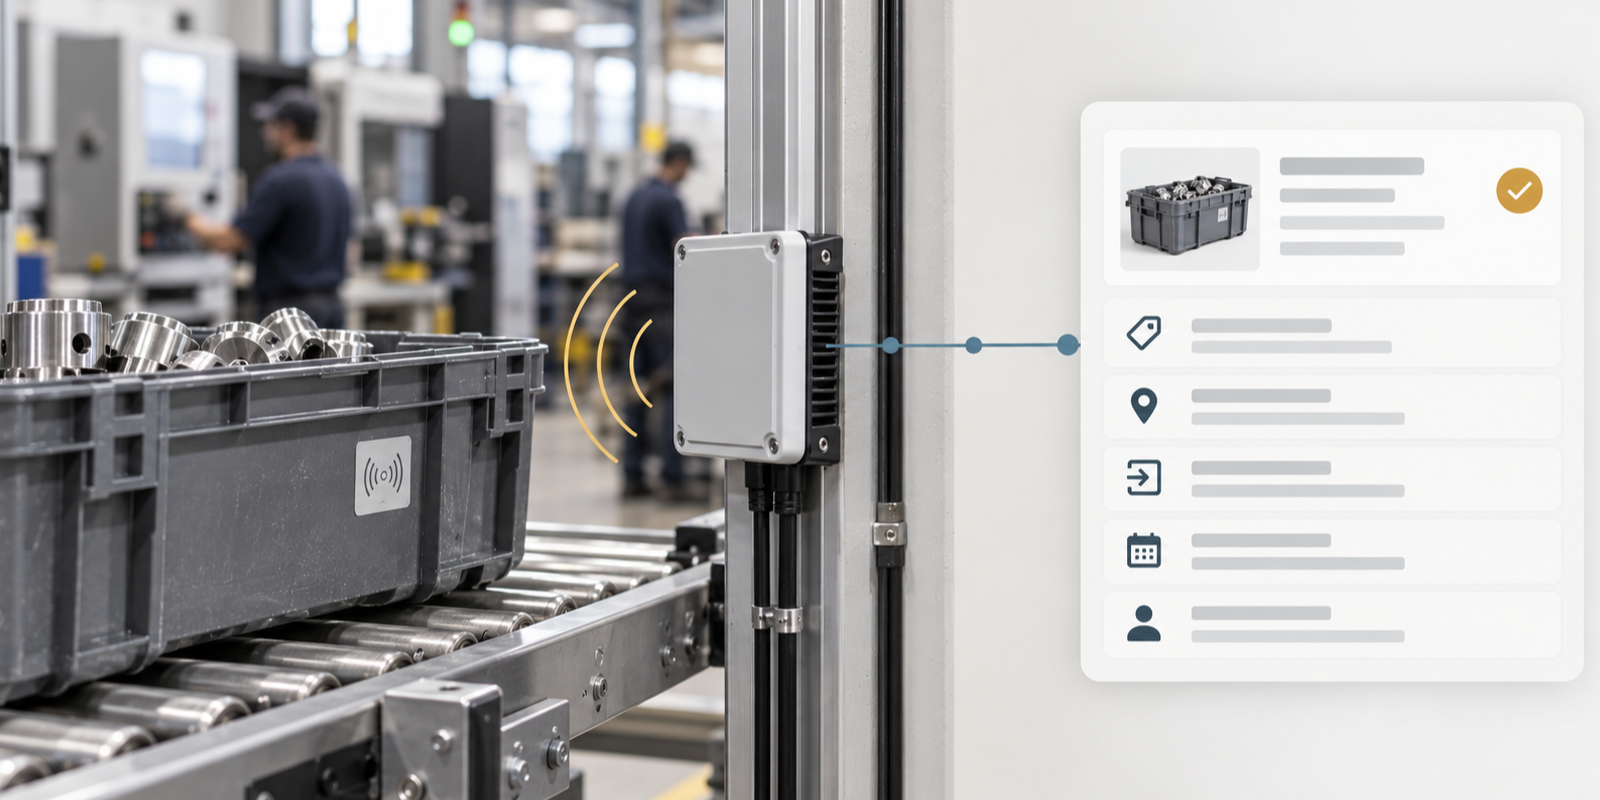
- Assets in industrial facilities are rarely gone. They are somewhere on site and nobody can say where, which is a different problem with a different solution and a cost that never reaches the profit and loss.
- The expense shows up as absorbed labor, replacement purchases coded to the wrong reason, and schedule delays booked as production variance. None of it is visible as a searching cost.
- Scale is what turns it from an inconvenience into a constraint. Across dozens of buildings, the question stops being what you own and becomes where it is.
In most large manufacturing sites, finding lost assets is a constant source of pain, cost, and delay. We see it on almost every facility survey we run. Walk a plant with the operations team and ask where things go missing, and nobody hesitates: they name the bay, the staging area, the outdoor yard, the second shift. The items themselves are rarely gone. They are on site, in one of a dozen places they could reasonably be, and the only way to find them is for somebody to stop what they are doing and go looking. Sometimes teams are lucky and go-finds are quick, but sometimes they can take days.
What surprises most people is how little of that cost is recognized by management without a tool to measure it. The searching is real, the delays are real, and the second purchase orders are real, but none of them arrive on leadership's desk labeled as what they are.
Where the cost of lost assets lives
It appears in three places, none of them labeled.
The first is absorbed labor. When a technician spends twenty minutes finding a tool, that time is paid for inside a shift that was going to happen anyway. Nothing is recorded, nobody reports it, and the cost is invisible precisely because it never becomes an exception. Multiply it across a workforce and a year and the number is substantial, but it exists only as a general sense that things take longer than they should.
The second is replacement purchasing. Items get bought again because they could not be found, and the purchase is coded to the category of the item rather than to the reason. Finance sees consumption; nobody sees duplication. In facilities that track this properly after the fact, a meaningful share of replacement spend turns out to have been for equipment that was on site the whole time.
The third is schedule. Work that waits on material which is somewhere in the building is recorded as a production variance, an efficiency number, or a late delivery. The cause is a location failure and the symptom is booked as an operational one, which is why the two are almost never connected in a management report.
What scale does to the problem
In a single building with one stores area, a misplaced asset is usually an inconvenience. Someone eventually remembers where it was left, and the problem resolves itself. FactorySense occasionally works with smaller manufacturers where this kind of informal process still functions reasonably well, and the solution can be relatively simple.
At campus or enterprise scale, however, asset-location problems become structural. Our deployment with Northrop Grumman at Space Park illustrates the difference. The site spans approximately 1.5 million square feet across 46 buildings. At that scale, no one can keep track of the location of thousands of assets from memory, and the informal systems that work in a single building begin to break down.
The question changes from "what do we own?" to "where is it now?". Traditional inventory systems are generally designed to answer the first question. They are much less capable of continuously answering the second.
The Space Park deployment was named runner-up in the RFID Journal 2024 Awards for Best Large-Scale Deployment, and FactorySense presented the project jointly with Northrop Grumman at the conference. The full story is available in our write-up of that award.
RFID usually comes after other fixes have been tried
Most organizations have already tried three things before they look at RFID.
They have tightened the sign-out process, which works while attention is on it and decays within a quarter, because the discipline depends on people doing something that slows them down. They have run an audit, which produces an accurate picture on the day and an increasingly inaccurate one thereafter. And they have treated it as a security problem, which leads to spending on cameras and access control and does not help, because in industrial settings the overwhelming majority of items that cannot be found have not been stolen.
What these have in common is that they ask people to maintain a record, but human processes are the thing that typically cause assets to go missing in the first place.
What changes
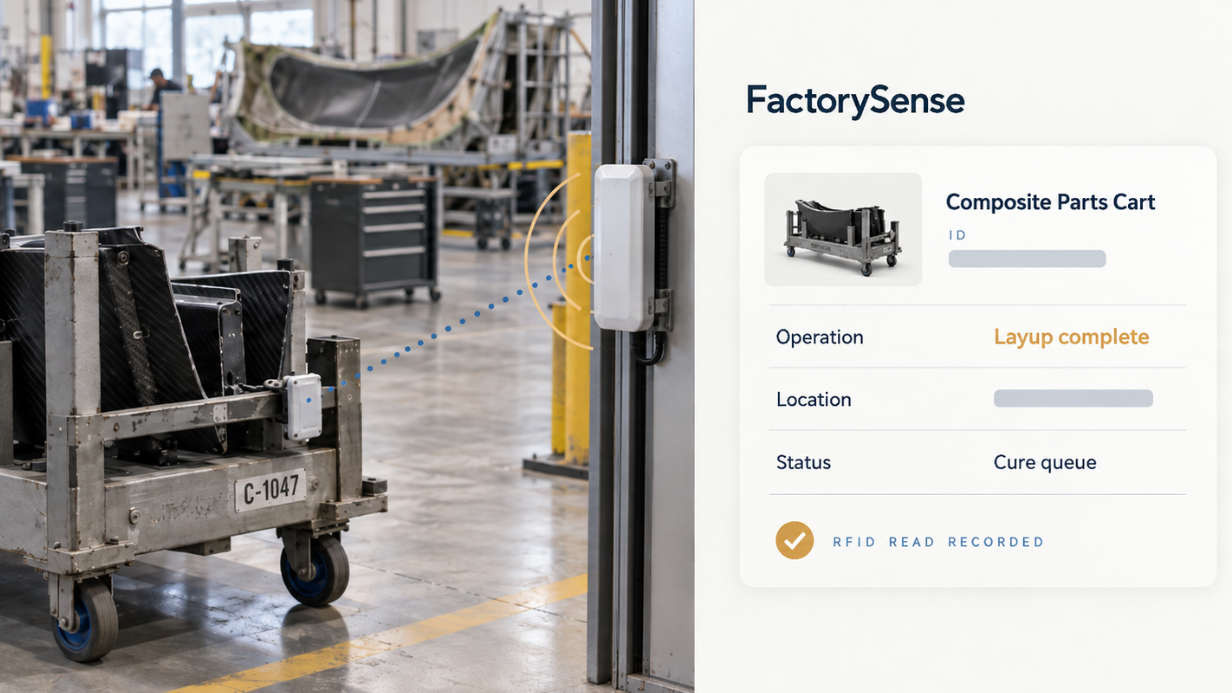
Automatic identification removes the reporting step. An item passing a fixed reader generates a record without anyone deciding to create one, which means the location history is a by-product of movement rather than an act of administration. When connected to your ERP system, that location is updated live in your system of record immediately without the need for any employee to take any action whatsoever.
In practice that splits into two capabilities. Fixed readers at doorways and transition points tell you where something went, which is what you need when the item could be anywhere. Handheld readers tell you where something is now, narrowing a search in a defined area far faster than walking and asking. Most deployments need both, and the balance between them is a design decision rather than a product one. Our asset tracking guide covers how that works.
The same approach applies to equipment carrying a time obligation as well as a location one. In our work with an industrial equipment manufacturer, the problem was not only finding calibrated tools but knowing whether each one was still inside its calibration window, which is an audit finding rather than an inconvenience when it is wrong.
Northrop Grumman gains efficiency and reduces asset loss
Work order and asset tracking across 46 buildings at the Space Park campus, where manual methods had stopped scaling. Runner up, RFID Journal 2024 Awards.
Read the case studyDigitizing asset and calibration tracking at scale
Locating calibrated tools and knowing whether each remained inside its calibration window, where being wrong is an audit finding rather than an inconvenience.
Read the case studyRFID is not a cure-all
RFID will not find an item that was never tagged, and deciding what should be tagged requires thought, experience, and documented processes. It also cannot overcome a poorly designed read environment. Metal-dense areas, liquid-filled containers, and outdoor yards can all reduce performance, which is why tag selection and read-point placement should follow a site survey rather than a specification sheet.
RFID also cannot compensate for a process in which assets routinely move through unmonitored areas. A location history with unexplained gaps quickly loses credibility, and once users stop trusting the system, they stop relying on it.
None of these limitations is an argument against RFID. They are an argument for good system design. The technology matters, but the quality of the implementation matters more than the purchase itself.
What to ask your team
Two questions will tell you whether this is worth pursuing, and neither requires a vendor in the room.
Ask which areas of the plant they do not trust the numbers for. People answer immediately, they answer consistently, and the answer identifies where the cost is concentrated.
Then ask someone to record, for two weeks, how much time is spent looking for things. Not estimate it in a meeting. Record it. That single number is usually enough to settle whether the rest of the exercise is worth doing, and it becomes the baseline for the business case. We set out how to build that case in building a defensible RFID business case.
The next step
What it would take, and what it would return, depends on your buildings, your materials and how your people actually work rather than how the process document says they do.
Book a Facility Visibility Assessment and we will walk the areas your team named and come back with the read points, the tagging approach and the measured baseline.
Why does this cost not appear in our financials?
Because it is absorbed rather than recorded. Search time is paid for inside shifts that were already going to happen, replacement purchases are coded to the category of the item rather than to the reason it was bought, and delays caused by material nobody can locate are usually booked as production variance. The money is real; the line item is not.
Is this a theft problem?
Rarely, in an industrial setting. The overwhelming majority of items that cannot be found are still on site. Treating it as a security question leads to spending on security, which does not address the actual failure.
What does an executive need to decide?
Two things. Whether the cost is large enough to be worth measuring, which two weeks of observation will answer. And where to start, which should be the area your own team already distrusts rather than the area with the most expensive assets.
Schedule a complementary working session with an RFID professional to discuss your floor or yard, your systems of record, and where the visibility gap between them is costing you.
Book a session