Using RFID in Supply Chains: A Guide to Product Quality Management
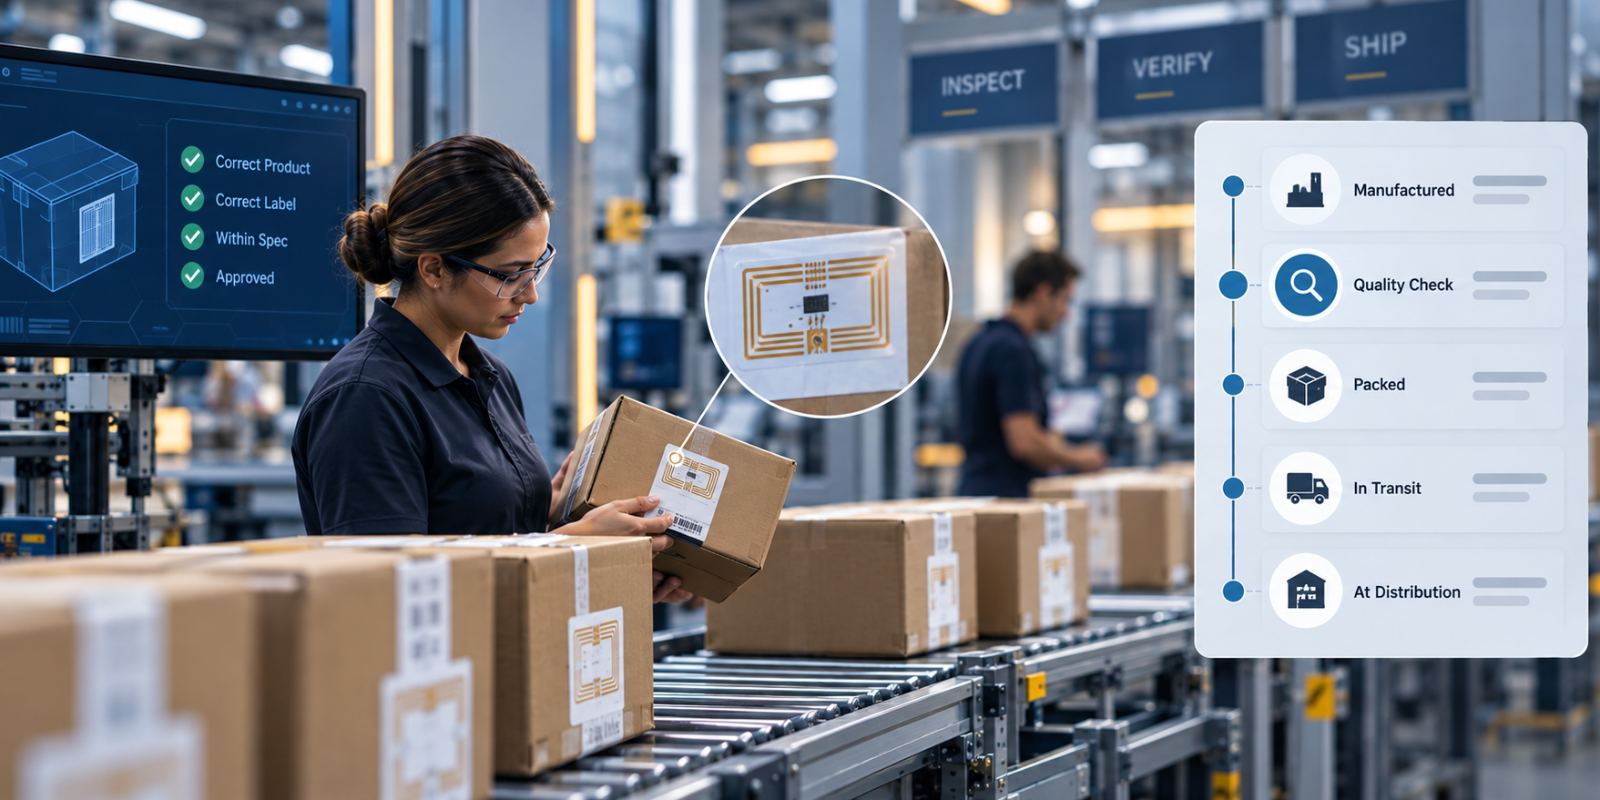
- RFID improves quality by making the point of failure locatable. If an item arrives damaged or out of tolerance, the read history shows where in the chain it happened.
- Many of the most practical applications are routine: receiving verification, correct kitting, missing component alerts, shelf life and tool calibration windows.
- Compliance regimes such as AS9100 and FDA requirements assume you can demonstrate after the fact what happened to a controlled item. An automatic read record is easier to produce at audit than a paper trail reconstructed after the fact.
Supply chain management in aerospace, pharmaceuticals and electronics has become harder. Geopolitical disruption, component price volatility and longer lead times mean more of the chain has to be monitored before you can set client expectations with any confidence.
Most discussion of RFID in this context is about knowing where things are. A less obvious application, and often a more valuable one, is quality. RFID will not prevent every defect, but it can show where in the chain a defect occurred.
Why locating the failure matters more than counting it
When an item arrives in unacceptable condition, the expensive question is where the problem happened. Without a read history, the supplier, carrier and manufacturer are left to argue about it. With one, they can trace it.
A tamper-evident tag on a pharmaceutical shipment is a useful illustration. If the tag shows mishandling in transit, the problem is in the logistics chain. If it does not, the manufacturer should look at its own on-site quality control. Either answer points to something specific to fix, and both depend on the record existing.
The same logic applies across the chain. When you can identify the batch, supplier or operation that introduced a fault, quality management can run continuously instead of waiting for a periodic audit.
Where it actually gets used
The applications that see the most use are routine and specific.
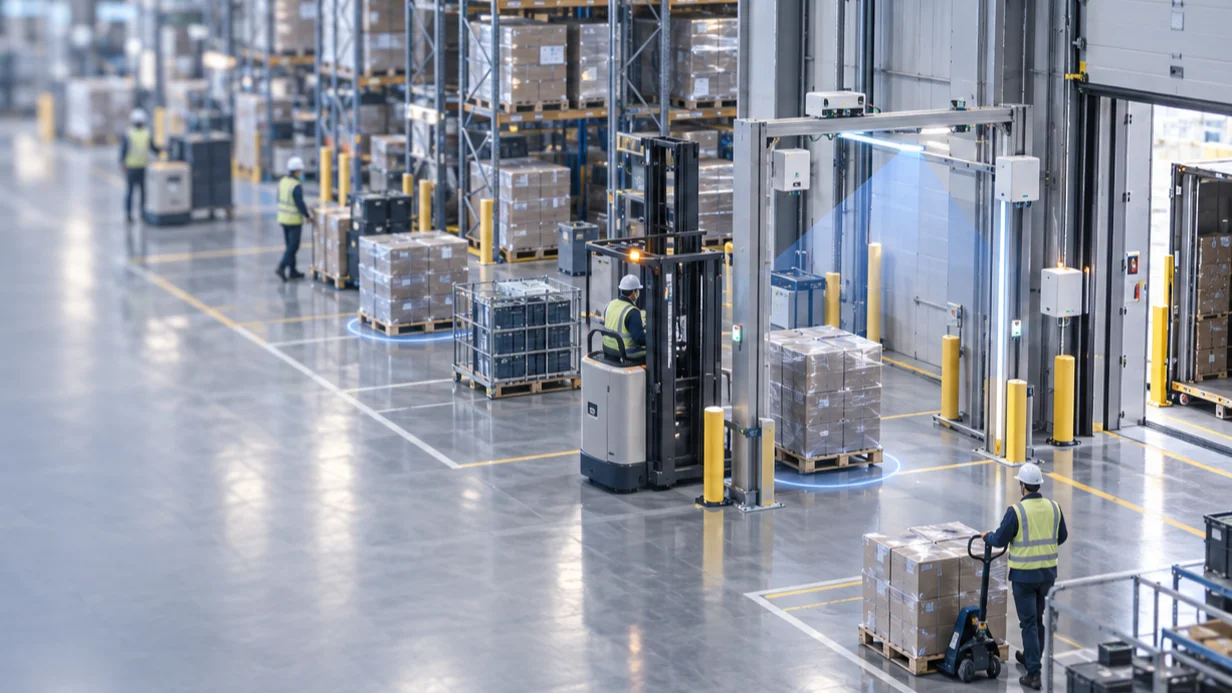
- Receiving verification. Checking an inbound shipment against the purchase order automatically, so discrepancies are caught at the dock before material reaches the line.
- Correct kitting. Confirming that the components picked for a production batch are the right ones before the batch starts, so a substitution does not surface downstream.
- Missing component alerts. Flagging an absent item when it is needed, before its absence stops production.
- Tool management. Making sure tools are not left inside large assemblies. In aerospace, a tool left behind is a foreign object debris problem.
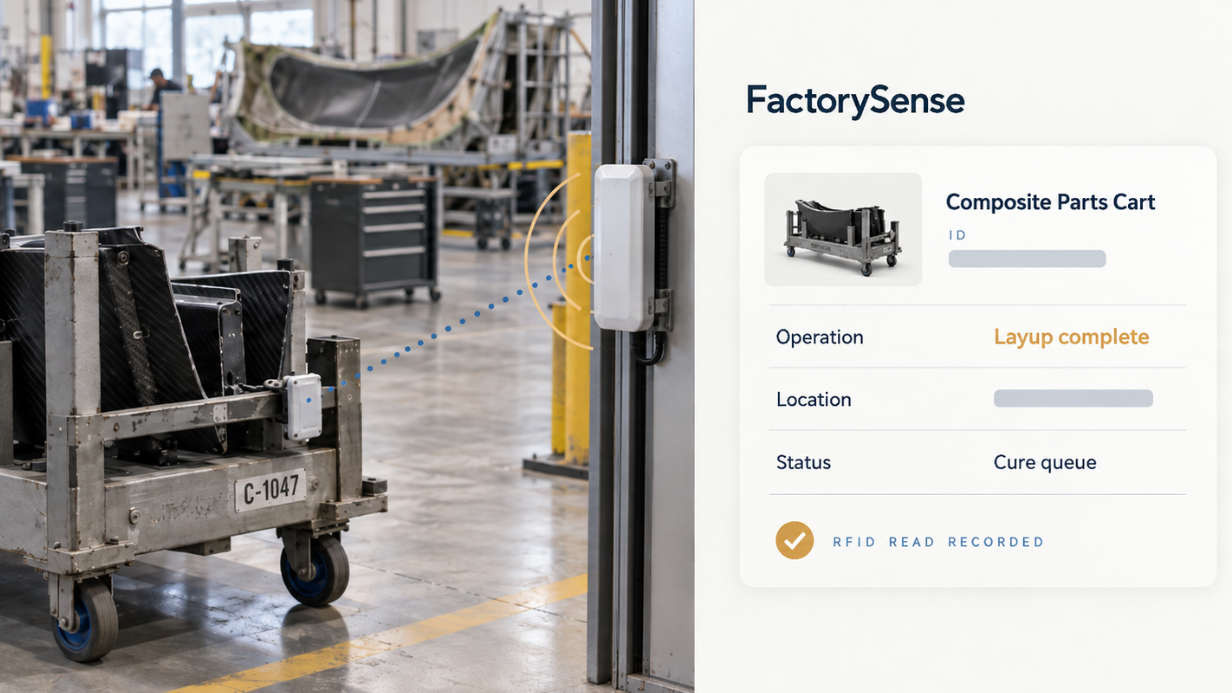
- Shelf life and out-time. Monitoring time-sensitive materials so they are used inside their window. In composites, material used outside its window can mean a scrapped part.
- Calibration windows. Tracking whether a tool is inside its calibration period. In an AS9100 environment, using a tool outside that period becomes an audit finding.
Each of these is a rule about a physical object that somebody currently enforces by remembering to check. Automatic identification lets the system enforce it instead.
Compliance is about evidence
Pharmaceutical manufacturers work to FDA requirements, aerospace manufacturers to AS9100, and defense suppliers to DFARS and ITAR obligations. All of these assume that an organization can demonstrate, after the fact, what happened to a controlled item and who handled it.
That evidence can be assembled from paper records and system exports, but it takes time. A read history makes it considerably faster to produce. For most manufacturers, the compliance case for RFID is about reducing the cost of proving conformance.
Integration is what makes it useful
Read data that stays inside a separate tracking tool has limited use. It becomes useful when a read becomes a transaction in the ERP or MES, so quality holds, batch releases and supplier scorecards draw on the same record as production.
That integration is also where most of the work sits. Choosing hardware is a contained decision, while mapping read events to business rules is open-ended and depends on how the business already runs.
What a deployment needs
A deployment needs four things, listed roughly in order of difficulty: consulting to establish what should be tracked and why, hardware appropriate to the environment, software that connects tag data to the systems of record, and support that continues after go-live.
Choose a partner with a record in your industry specifically. Quality requirements in aerospace, pharmaceuticals and electronics differ enough that experience in one does not transfer cleanly to another.
Related reading
For a worked example in calibrated equipment, see our asset management and calibration case study. For how the underlying data layer is built, see how manufacturers connect real-time factory data to business systems.
The next step
Which quality rules are worth enforcing automatically depends on where your chain fails. Your team usually knows where that is, even if it is rarely written down. Book a Facility Visibility Assessment and we will work through it against your operation.
How does RFID help with quality rather than just location?
RFID records where and when an item was. When a quality failure occurs, that history lets the supplier and manufacturer trace it to the point in the chain where it happened and work from the record.
What does RFID do for shelf life and calibration?
Both are time-based rules applied to a physical item. Once the item carries an identity that is read automatically, out-time on composites or a calibration window on a tool can be enforced by the system without relying on someone to check a log.
Does this help with AS9100 or FDA requirements?
It helps with the evidence, which is usually the expensive part. Both regimes assume you can demonstrate after the fact what happened to a controlled item. An automatic read record is easier to produce at audit than a reconstructed paper trail.
Schedule a complementary working session with an RFID professional to discuss your floor or yard, your systems of record, and where the visibility gap between them is costing you.
Book a session