Real-World RFID Examples: 6 Industrial Deployments and What They Show
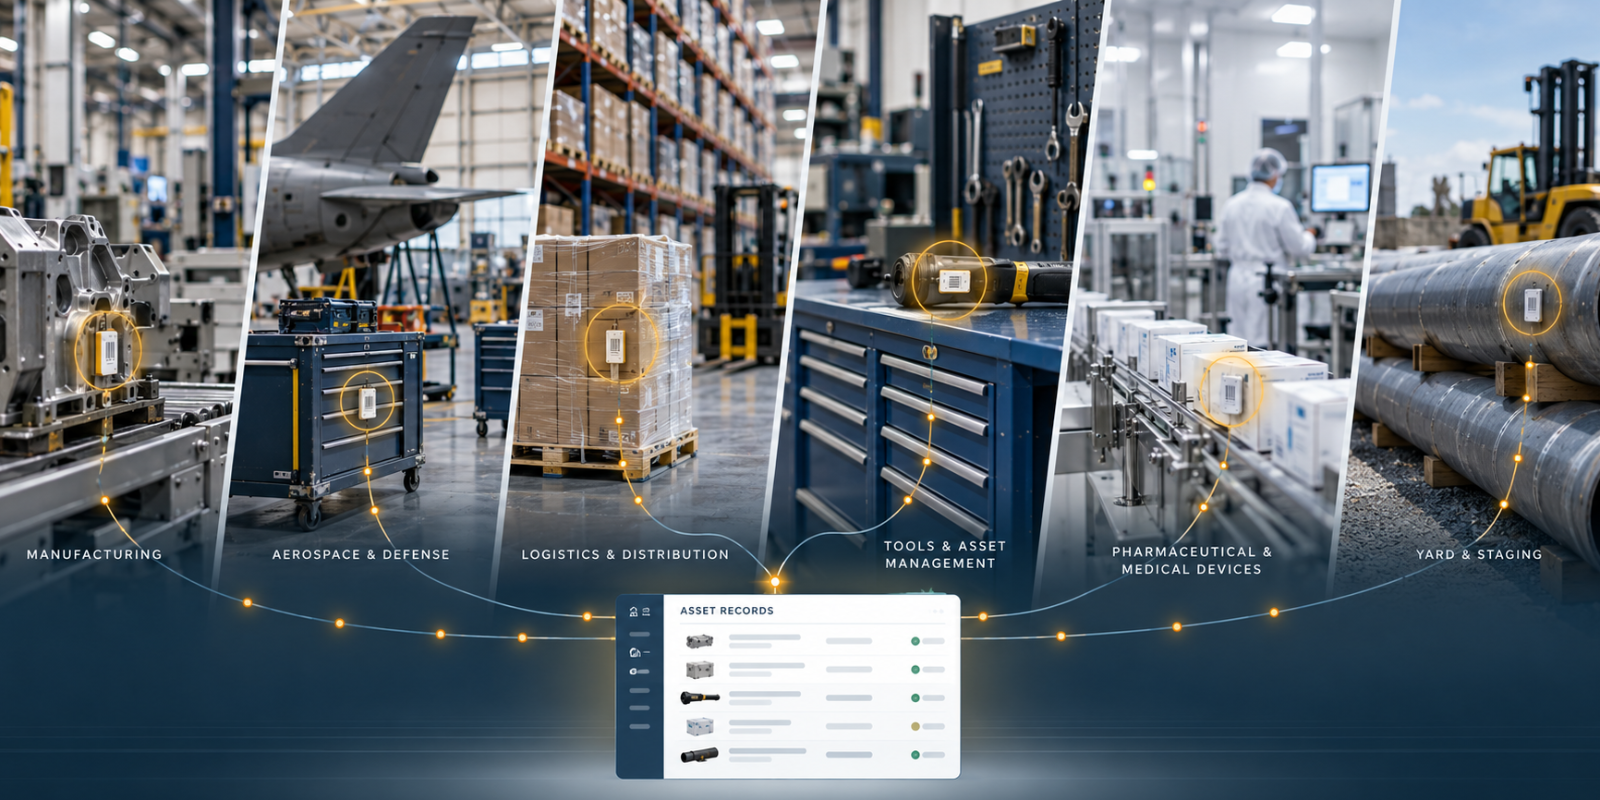
- Real RFID deployments start with different operating problems: WIP handoffs, asset search, tooling, calibration, labeling, inventory capture or regulated traceability.
- The common architecture is physical identity, a meaningful observation point, event logic and integration with the system that owns the business record.
- The most useful comparison case is often one with the same workflow problem, even if it comes from another industry.
Most RFID articles describe use cases as a list: inventory, assets, work-in-process, tools, logistics and compliance. That is useful at a high level, but it does not show what changes when the technology meets a real operating process. The examples below are drawn primarily from FactorySense deployments because they show the object being tracked, the problem that existed before RFID and the architecture that was actually used.
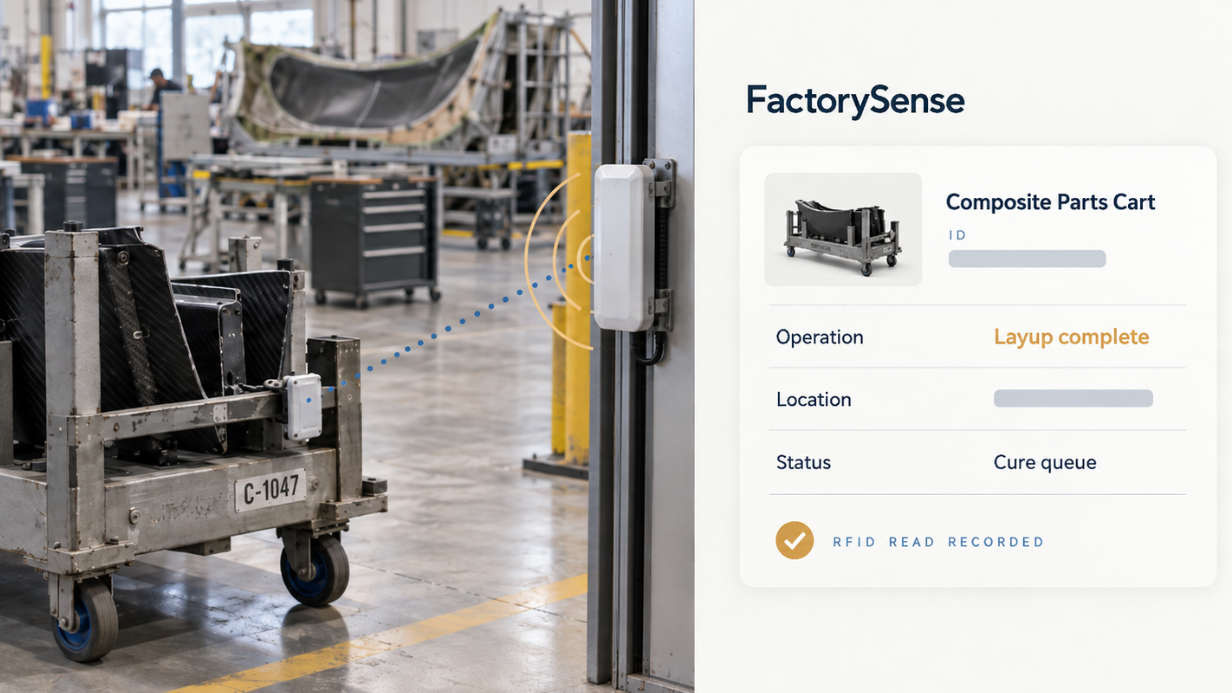
What the projects share is a link between a physical observation and a business event that matters, whether that event is an assembly entering a production area, a tool returning to a crib, an asset appearing in another building or a compliant label being produced for a retail customer. That physical-to-digital handoff is also consistent with NIST's digital-thread work, which treats manufacturing visibility as part of a larger flow of product, process and quality information.
Six real-world RFID deployment patterns
| Deployment | Problem | RFID pattern | Main lesson |
|---|---|---|---|
| Northrop Grumman | Finding assets across a large aerospace campus | Fixed + handheld asset tracking | Last-seen history and search can matter more than continuous coordinates |
| Honeywell Aerospace | Unreliable WIP visibility | Passive RFID at production handoffs | Event quality matters more than tag sophistication |
| Global industrial manufacturer | Tool search and calibration control | Passive RFID + BLE + calibration software | Location and calibration are related but distinct records |
| Louis Garneau | Retail RFID labeling requirements | RFID print and edge integration | RFID can be added without rebuilding the ERP workflow |
| Tier 1 automotive manufacturer | Skipped or unreliable manual scans | Fixed + handheld passive RFID | Automation is valuable when the capture step is the bottleneck |
| Medical-device manufacturer | Manual WIP tracking in a regulated environment | RFID checkpoints + ERP integration | RFID can strengthen traceability without becoming the quality system |
1. Northrop Grumman: finding assets across massive campus
At Northrop Grumman's Space Park campus in Redondo Beach, the tracking problem was scale. The aerospace campus covers more than 1.5 million square feet across 46 buildings, so locating high-value assets with traditional methods could consume meaningful time even when the asset was still somewhere on site. FactorySense implemented a combination of fixed and handheld RFID, software integration and a standardized tagging strategy across varied operating environments.
The Northrop Grumman case study is a useful counterexample to the idea that every asset-tracking project needs a continuous live coordinate. Fixed observations can build movement history, while handheld readers can help a worker search the last known area when an item is not where expected. Our asset-tracking guide explains why last seen, search and repeated location should be treated as different requirements.
A large campus does not need uniform infrastructure everywhere. Coverage can follow the cost of uncertainty, the movement patterns of each asset class and the locations where a read has operational meaning, which usually scales better than trying to turn every square foot into a continuous location system.
2. Honeywell: rebuilding WIP tracking around trustworthy events
Honeywell Aerospace already had RFID before FactorySense became involved. The legacy active-tag system created battery-maintenance burden, inconsistent data and coverage problems, which meant the plant had technology but still lacked WIP information it could trust. FactorySense reassessed the tag performance, reader placement, software and integration model, then moved the application to passive RFID at controlled production points.
The Honeywell case study treats WIP tracking as an event-design problem. A read at a production boundary can support a state change when the software knows the object, the read point and the expected process context. The FactorySense WIP guide covers that distinction between raw reader observations and meaningful production events.
Once the production data became dependable, the infrastructure expanded to carts and tooling. That order is a practical way to scale RFID: prove one event model, earn trust in the data, then reuse the identity and reader infrastructure for adjacent asset populations. The scope grew because the first workflow worked.
3. Industrial tooling: combining location with calibration status
A global heavy-equipment manufacturer had two related problems with calibrated assets. Teams spent time locating tools, while calibration status was managed through separate processes and software. FactorySense deployed durable RFID tags, BLE where wider-area visibility was useful, fixed read points at tool cribs and calibration areas, handheld search and software that joined asset location with calibration records.
The calibration and asset-management case study keeps tracking and status separate even when users see them on the same screen. RFID can establish where a tool was observed or whether it crossed a controlled boundary, while the calibration-management record determines whether the tool is eligible for use. Our calibrated tool management workflow is built around that separation.
This pattern applies well beyond metrology tools. Maintenance equipment, test sets, gauges, fixtures and shared production assets can all benefit when physical location is connected to a business status that already exists elsewhere. RFID creates the physical evidence, while the appropriate asset or quality system continues to own the governing state.
4. Louis Garneau: meeting RFID labeling requirements without replacing the ERP
Louis Garneau came to RFID from a different direction. The sports-apparel manufacturer needed to meet retailer RFID labeling requirements across operations in Canada, Mexico and other locations without disrupting its existing workflow. FactorySense added RFID printers and edge integration so the company could produce GS1-compliant RFID labels without rebuilding its core business systems.
The Louis Garneau case study shows RFID value starting at the labeling boundary. RFID can enter an operation through print and encode workflows first, then become useful later for inventory or movement visibility. GS1 likewise treats RFID as one data carrier within a broader identification system that still includes printed identifiers.
The implementation also shows why integration does not always have to begin as a large ERP project. An edge layer can intercept or transform the information already being produced by the business process and add the RFID encoding required by the downstream customer. Our integration guide discusses the same principle more broadly: physical data should meet the enterprise system at the right boundary, so the enterprise system never has to understand reader hardware.
5. Automotive manufacturing: replacing a capture step that people could skip
At a Tier 1 automotive manufacturer, barcode scans and handwritten logs were producing delayed and incomplete inventory records. Barcodes could identify the items. The trouble was that the transaction depended on a manual capture step that was routinely skipped, misread or completed after the physical movement had already occurred.
FactorySense deployed passive RFID on selected inventory units and subassemblies, fixed readers at key transitions and handheld readers for spot checks and search. The automotive manufacturing case study therefore illustrates one of the clearest reasons to move from optical scanning to RFID: the physical flow has enough volume that the individual scan itself becomes the weak point. The RFID-versus-barcode decision should be made process by process.
A good RFID assessment therefore begins by observing where the digital record falls behind the floor. If a deliberate scan is useful and reliably performed, barcode may remain the better answer. If the scan adds labor or is routinely missed, automatic RFID capture can remove the failure point altogether.
6. Medical-device manufacturing: adding physical events to a regulated traceability record
A multinational medical-device manufacturer used manual methods, including barcodes and handwritten records, to track work-in-process through a regulated production environment. FactorySense introduced tagged WIP, fixed readers at selected checkpoints, handheld verification and ERP integration so physical movement could be captured with less manual intervention. The medical-device case study shows how RFID can strengthen the physical history without becoming the regulatory record by itself.
Medical-device identification already sits inside formal requirements. The FDA's UDI system requires covered device labels and packages to carry identifiers in human-readable and machine-readable AIDC form, but it does not make RFID mandatory for every device or manufacturing process. RFID can support internal WIP visibility and identity capture while the quality system, UDI process and ERP continue to own their respective records.
The same caution applies across regulated deployments: a reader observation should not be promoted into proof of inspection, sterility, calibration or acceptance unless the governing process provides that evidence. RFID works best there when it reduces the effort of capturing the physical event and leaves engineering and quality decisions with the processes that own them.
What these projects have in common
These six deployments look different because the physical problems are different, but the architecture follows the same sequence. First, an object gets a durable identity that the business can resolve. Second, a reader observes that identity at a place or moment with operational meaning. Third, software turns the observation into an event the enterprise can use.
GS1's EPCIS standard describes visibility data in similar terms: what object was involved, when something happened, where it happened and the business context for why the event matters. FactorySense systems do not require customers to implement EPCIS, but the standard is a useful conceptual model because it separates a raw identifier from a meaningful business event. Every case above makes that separation, including those where the customer uses its own event model.
The projects also show why the hardware list is rarely the best place to start. Northrop Grumman needed campus-scale search, Honeywell needed trustworthy WIP transitions, the tooling customer needed location plus calibration context, Louis Garneau needed a label workflow, and the automotive customer needed to eliminate missed scans. In each case the architecture followed from that operational question.
How to use these examples when evaluating your own project
Look for the closest operational pattern rather than the closest industry. A defense plant looking for shared test equipment may have more in common with the industrial calibration case than with another defense logistics project. A medical manufacturer with invisible WIP may have more in common with Honeywell's production flow than with a hospital asset-tracking deployment.
Then define the first event worth automating. The pre-installation guide explains how to test the real tag, object, read point and integration before scaling. A pilot should prove that one physical event becomes a trustworthy business event with less effort than the current process.
A successful RFID deployment removes a source of uncertainty or manual work that already matters to the operation, and each of these case studies starts from a problem of that kind.
If one of these examples resembles your operation, these pages go deeper: RFID asset management, RFID work-in-process tracking and RFID inventory management. For aerospace specifically, see RFID tracking in aerospace manufacturing. The Northrop Grumman Space Park project was also runner up in the RFID Journal 2024 Awards for best large-scale deployment.
What are the most common real-world RFID applications?
Common industrial applications include work-in-process tracking, asset and tool location, inventory movement, returnable-container tracking, calibration workflows and RFID label compliance. The architecture varies depending on whether the business needs a transition event, last-seen location, search or repeated location.
Do successful RFID projects replace existing ERP or quality systems?
Usually not. RFID provides physical identity and movement observations, while ERP, MES, QMS, calibration or maintenance systems remain authoritative for the business state. Integration turns the RFID observation into useful operational data.
Which RFID case study should I compare with my project?
Choose the case with the closest process problem rather than the closest industry. A manufacturer searching for calibrated tools may learn more from another tool-control deployment than from a generic case in its own sector.
Schedule a complementary working session with an RFID professional to discuss your floor or yard, your systems of record, and where the visibility gap between them is costing you.
Book a session